Products / Diamond & CBN Tools / Diamond Grinding Wheels

CUSTOM DIAMOND TOOL GRINDING WHEELS
Resin Bond Diamond Cup Grinding Wheels for Carbide Tools
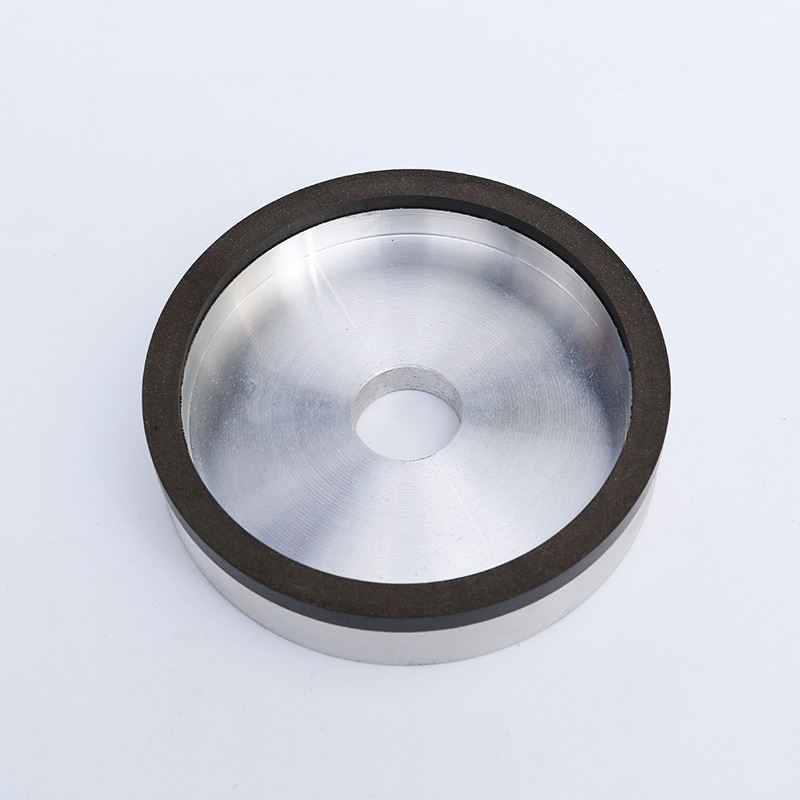
Resin bond diamond cup grinding wheels are used for precision face, edge and sharpening operations on cemented-carbide tools. This Cup-Type B series has a machined metal body, a continuous diamond rim and six listed diameters from 100 to 200 mm. Final grit, concentration, dimensions and operating speed are confirmed for the machine and grinding target.
100–200 mm listed diameter · 75% listed concentration · Made to order
Product Overview
The cup profile provides a recessed metal body and a continuous diamond rim for face, edge and tool-grinding access. The listed configurations use a resin-bond sintered diamond layer. Final grit, concentration, bond specification, dimensional tolerance, balance and maximum operating speed must be confirmed for the workpiece, spindle and grinding process before production.
Key Product Features
- Resin-bond diamond abrasive rim
- Machined metal cup body
- Continuous peripheral grinding layer
- Six listed dimensional configurations
- Custom grit and alternative concentration available
- Drawing-based customization for industrial grinding
Listed Dimensions
Dimension order used on this page: D × T × H × W × X, in millimetres. Listed weights are approximate and must not be used as shipping weights until the final drawing and specification are confirmed.
| Catalog size (D × T × H × W × X) | D Outside diameter | T Body height | H Bore | W Diamond rim width | X Diamond layer height | Approx. weight |
|---|---|---|---|---|---|---|
| 100 × 32 × 20 × 10 × 3 mm | 100 mm | 32 mm | 20 mm | 10 mm | 3 mm | 120 g |
| 125 × 32 × 32 × 5 × 3 mm | 125 mm | 32 mm | 32 mm | 5 mm | 3 mm | 320 g |
| 125 × 32 × 32 × 10 × 3 mm | 125 mm | 32 mm | 32 mm | 10 mm | 3 mm | 380 g |
| 150 × 35 × 32 × 5 × 3 mm | 150 mm | 35 mm | 32 mm | 5 mm | 3 mm | 560 g |
| 150 × 35 × 32 × 10 × 3 mm | 150 mm | 35 mm | 32 mm | 10 mm | 3 mm | 580 g |
| 200 × 40 × 32 × 10 × 3 mm | 200 mm | 40 mm | 32 mm | 10 mm | 3 mm | 1,180 g |
Dimension note: D is outside diameter, T is total body height, H is bore diameter, W is abrasive-rim width and X is abrasive-layer height. Non-listed dimensions are subject to drawing review.
Technical Specification
| Item | Listed / Confirmation Basis |
|---|---|
| Product form | Cup-Type B diamond grinding wheel |
| Abrasive | Diamond |
| Bond and process | Resin bond; sintered construction |
| Listed concentration | 75%; other concentrations available for customization |
| Grit | Custom; select for stock removal, edge quality and surface-finish target |
| Listed availability | Made to order; confirm quantity and lead time |
| Maximum operating speed | Must be confirmed in writing for the final wheel drawing and machine |
| Coolant / dry use | Confirm for the actual process |
| Balance, runout and dimensional tolerance | Confirm on the approved drawing |
Typical Applications
Carbide Tool Grinding
Face, edge and sharpening operations for suitable cemented-carbide tools after the wheel geometry and grit are matched to the machine.
Hard, Brittle Materials
Application-reviewed grinding of suitable technical ceramics, stone and other hard non-ferrous materials.
Custom Tool-Grinder Setups
Drawing-based wheel dimensions for compatible tool grinders where cup access and a continuous diamond rim are required.
Customization and RFQ Information
- Workpiece material, grade and hardness
- Grinding operation and stock removal
- Machine model, spindle interface and speed range
- Required D, T, H, W and X dimensions
- Grit, concentration and surface-finish target
- Wet or dry grinding and coolant
- Existing wheel marking, drawing or clear photos
- Trial quantity and annual requirement
Safety and selection note: do not install this wheel on a handheld grinder or any other machine until the final wheel specification, mounting interface and maximum operating speed have been confirmed for that machine. Diamond is normally selected for carbide and other suitable hard non-ferrous materials; use CBN for hardened ferrous materials unless the application has been specifically reviewed.
How to Select Resin Bond Diamond Cup Grinding Wheels
Select the wheel from the workpiece, grinding operation and machine—not diameter alone. Confirm the approved drawing and maximum operating speed before production or installation.
| Decision factor | Selection guidance |
|---|---|
| Workpiece material | Use diamond for cemented carbide and suitable hard, brittle non-ferrous materials. For hardened ferrous materials, evaluate CBN instead. |
| Grinding goal | State whether the priority is stock removal, edge quality, form holding or final surface finish; this determines the grit and bond review. |
| Wheel geometry | Match D, T, H, W and X to the spindle, guard, tool access and approved machine envelope. Use a straight or dish wheel when the cup profile does not provide suitable access. |
| Process conditions | Confirm spindle speed, wet or dry operation, coolant, feed, contact area and dressing method before the final specification is released. |
| Application limit | Do not use an unconfirmed made-to-order wheel on a handheld grinder. Operating speed, mounting interface, balance and runout must match the approved drawing. |
Related Products
Compare two related resin-bond diamond wheel profiles for different tool access and grinding requirements.
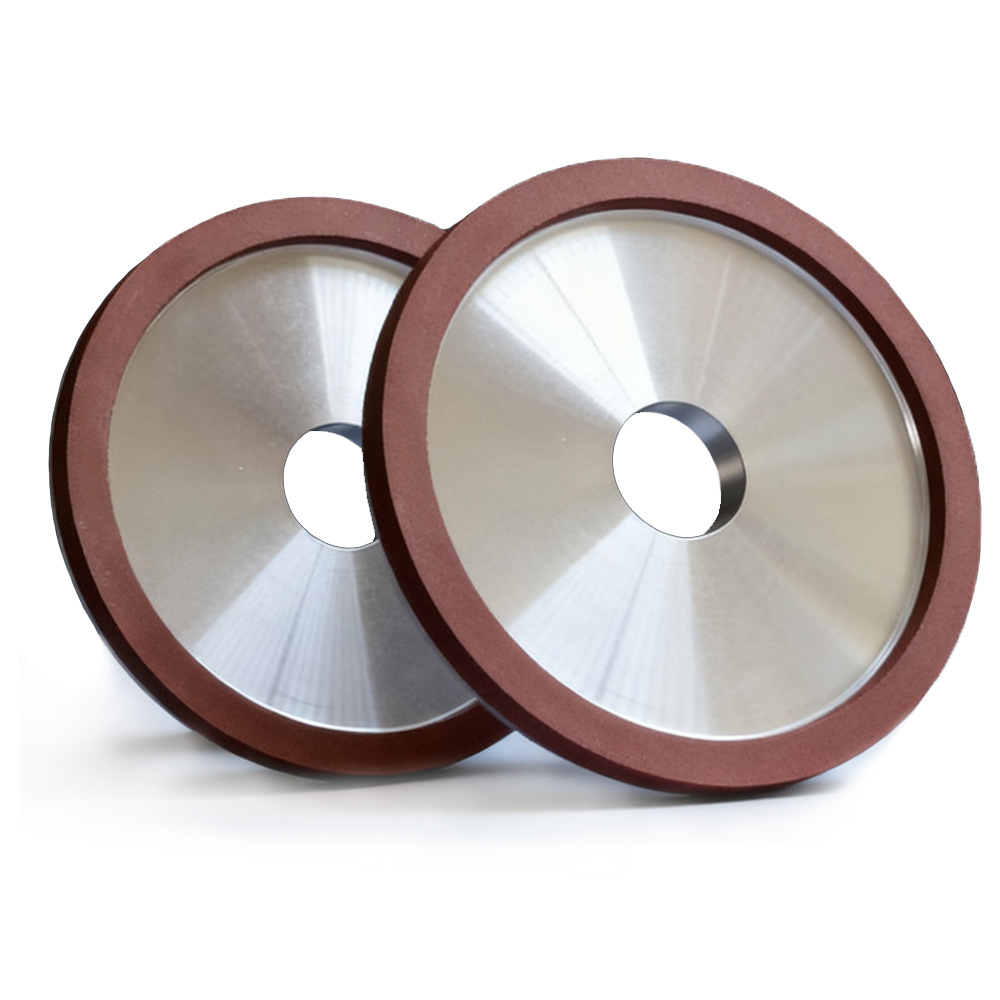
Resin-Bond Diamond Dish Grinding Wheels
Dish-profile wheels for carbide tool grinding where recessed access and controlled edge clearance are required.
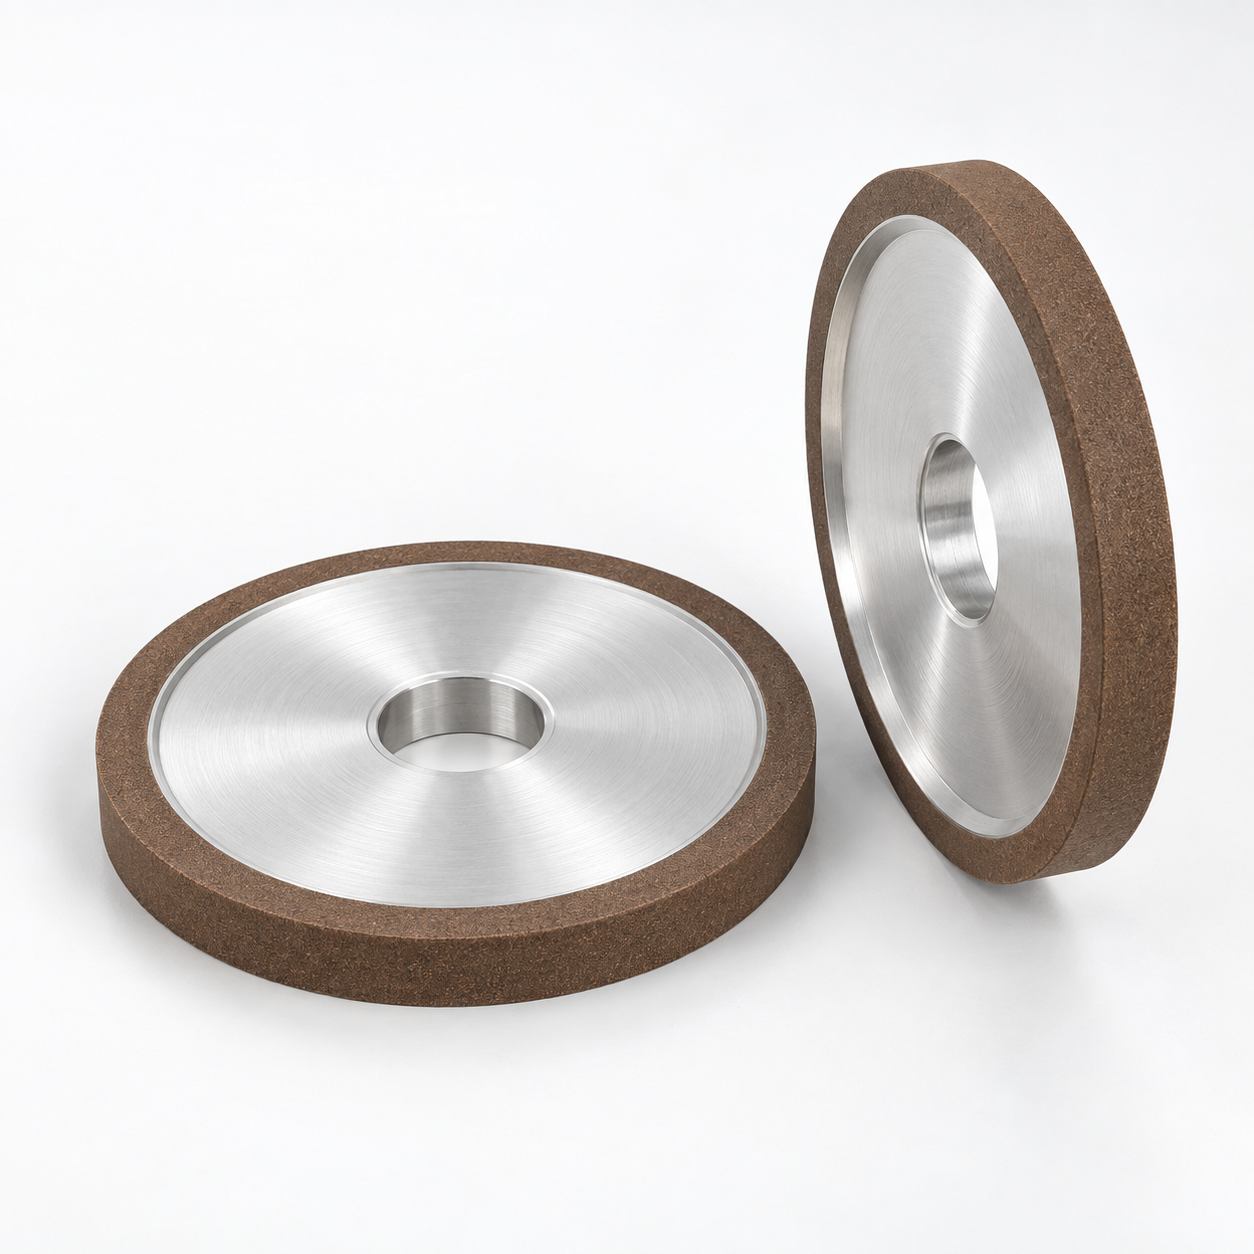
Resin-Bond Diamond Straight Grinding Wheels (1A1)
Straight wheels for surface, cylindrical, plunge and form grinding of suitable cemented-carbide tools and components.
Related Resources
Browse all Diamond Grinding Wheels
Read: CBN vs Diamond Grinding Wheels—Material Selection Guide
Send Your Wheel Drawing and Grinding Conditions
Send the catalog size or drawing, workpiece material, machine speed and required grinding result. We will review the geometry and confirm the final specification before quotation.